A manufacturing traceability system connects the history of a product to the materials, suppliers, production activities, quality checks and dispatch records behind it. Instead of searching through separate spreadsheets, paper forms and warehouse documents, a factory can follow a material lot forward into finished products or trace a finished batch backward to its original inputs.
For Saudi manufacturers, traceability is an operational capability, not simply a reporting feature. It helps teams investigate quality issues, manage supplier problems, respond to customer questions and maintain reliable production records. A well-designed [manufacturing ERP system]( /erp-crm/manufacturing/) can connect these records across purchasing, inventory, production, quality and sales rather than treating traceability as an isolated application.
What a manufacturing traceability system should track
Traceability means being able to establish what happened to a material or product, where it moved, which process handled it and what records were created along the way. The exact information depends on the factory's products and processes, but most manufacturers need to connect several types of records.
- Supplier and receiving information: supplier identity, purchase order, delivery reference, material description, received quantity, receipt date and supplier lot or batch number.
- Internal material identity: the factory's own lot number, storage location, inspection status and any relabelling or splitting of the original delivery.
- Production consumption: the production order, batch, line, work centre, operator record where required, and the quantities of materials issued or consumed.
- Process and quality records: inspection results, process checks, nonconformances, rework, approvals and relevant equipment or environmental records.
- Finished-product identity: product code, batch or serial number, production date, packaging reference, quantity and release status.
- Dispatch and customer records: delivery note, shipment date, destination, customer order and the finished batches included in the shipment.
The objective is to connect these records with consistent identifiers. A lot number printed on a receiving label should remain meaningful when material is moved, reserved, consumed, transformed, packed or dispatched.
Forward traceability: from supplier delivery to customer
Forward traceability answers a practical question: where did a particular supplier lot go after the factory received it?
Imagine that a factory receives a delivery of packaging material. The receiving team records the supplier, purchase order, delivery reference and supplier's lot number. The factory assigns an internal lot identifier if its process requires one, prints a label and places the material in an identified warehouse location.
When production requests the material, the warehouse issues a specific quantity against a production order. The system records which lot was issued, how much was consumed, whether any quantity was returned and whether the remaining balance is still available. If the material is used across several production batches, the relationship between the source lot and each batch must remain visible.
After production, finished goods receive their own batch or serial identity. Packaging and dispatch records connect those finished units to customer orders and shipments. The factory can then search for the original supplier lot and identify the production batches and deliveries associated with it.
A manufacturing traceability system should make this chain searchable without requiring employees to reconstruct it manually from unrelated documents. The system does not create reliable history simply because a lot number exists. Each important movement and transformation must be recorded as part of the normal operating workflow.
Backward traceability: from finished product to raw materials
Backward traceability starts with a finished product, batch or shipment and follows its history in reverse. A customer may report a product defect, a quality team may identify an issue during inspection, or a supplier may notify the factory about a material concern.
The investigation needs to establish which raw materials were used, which supplier lots supplied them, when the product was manufactured, which production order and line were involved, and what quality checks were completed. Depending on the process, the team may also need to examine packaging components, processing records, rework history and equipment maintenance records.
For example, a food manufacturer investigating a packaging complaint may need to identify the packaging-material lot, the production batches that consumed it and the customer shipments containing those batches. A metal fabricator may need to trace a finished component to a particular coil, sheet or heat reference and its inspection documentation.
A manufacturing traceability system should support both directions. Forward traceability helps identify where affected material went; backward traceability helps identify what went into a product. Together, they provide a more complete picture for investigation and containment.
Designing lot and batch identification
A traceability project often succeeds or fails at the point where identifiers are designed. If different departments use inconsistent codes, or if labels cannot be read reliably, even a sophisticated application will produce incomplete records.
Start by deciding what needs an identity. Depending on the operation, this may include:
- Purchased raw materials and ingredients.
- Packaging materials and consumables that affect product quality.
- Intermediate products and work in progress.
- Production batches, sub-batches and split quantities.
- Finished goods, pallets, cartons or individual serialized units.
- Returned materials, rework and quarantined stock.
Next, define the rules for creating, printing, changing and retiring identifiers. A supplier's original lot number should generally be retained as a reference, even when the factory creates its own internal code. If a received lot is divided across multiple locations or production orders, the system must preserve the relationship between the parent lot and its resulting quantities.
Avoid relying on a label format alone to represent the complete history. A barcode or QR code is a way to retrieve information; it is not the traceability record itself. The application behind the label must control the transactions and relationships that give the identifier meaning.
Connecting receiving, inventory and production
Traceability cannot stop at the warehouse door. Receiving, inspection, storage, material issue, production consumption, returns and finished-goods receipt all need to share the same item and lot records.
At receiving, employees should capture the required delivery details and identify material that needs inspection. If quality approval is required before use, the stock should remain in an appropriate status until the authorised decision is recorded. The warehouse team should not have to maintain a separate spreadsheet to remember which lots are on hold.
During storage and movement, the system should record the source and destination locations, quantity moved and relevant lot identity. Transfers between warehouses, production areas and external storage should preserve the same history. Where material is split, merged or repacked, the transaction should record the relationship rather than silently replacing the original identity.
At production issue, employees should scan or select the actual lot consumed, not simply confirm that a planned quantity was issued. The system should support substitutions when permitted, record actual consumption and capture returns or waste. These details matter because the planned bill of materials may not always match what was used on the production floor.
A connected manufacturing inventory management process provides the foundation for these transactions. Inventory accuracy and traceability reinforce each other: a lot history is only useful when the recorded quantities and locations reflect physical operations.
Quality management, holds and nonconformance
Quality records are an essential part of product history. A manufacturing traceability system should connect inspection outcomes to the relevant material lot, production batch or finished product instead of storing quality documents separately without a clear relationship.
A typical workflow begins when a delivery arrives. The quality team records the required inspection and decides whether the material can be released, rejected or held for further review. The system should make the status visible to purchasing, stores and production so that teams do not accidentally consume material awaiting approval.
During production, quality checks may be associated with a production order, batch, operation or sample. If a nonconformance is identified, the record should identify the affected quantity, its current location and the decision taken. Possible actions may include rework, additional inspection, controlled use, rejection or quarantine, subject to the factory's approved procedures.
Finished goods may also require release checks before dispatch. The system should prevent an unauthorised shipment when a required quality approval is incomplete. It should preserve the approval history, supporting documents and any authorised exceptions.
Software supports the workflow, but it does not define the factory's quality obligations. The manufacturer's quality and regulatory leads should confirm which checks, records, retention periods and release rules apply to each product and market.
What changes across manufacturing industries?
The traceability model should reflect the way a factory transforms materials. A single template rarely fits every production environment.
Food and beverage: Ingredient lots, packaging lots, recipes, production batches, processing records and finished-product dates may all need to be connected. Where ingredients are combined, the system should preserve the relationship between each input lot and the resulting batch. Rework and returned product need explicit handling rather than informal notes.
Plastics and packaging: Resin, additives, colour concentrates, films, inks and packaging components may be tracked by supplier lot and production run. Extrusion, moulding, printing or converting records can provide context for investigations. The factory should decide how to handle material blends, recycled inputs and production remnants.
Metal fabrication and building materials: Heat numbers, coil or sheet references, cement or aggregate batches, test certificates and cutting or processing records may be important. When material is cut into smaller pieces, the relationship to the original source should be retained where the process requires it.
Furniture and assembly: Components, purchased parts, hardware, upholstery or finish materials may be linked to a production order or assembled product. Serial tracking may be appropriate for selected products, while lot tracking may be sufficient for standard consumables.
These examples are design considerations, not a universal compliance checklist. The factory should identify which characteristics are necessary to investigate defects, satisfy customer requirements and operate its approved quality system.
Choosing the right technology: ERP, barcode, QR and shop-floor capture
A manufacturing traceability system can be delivered as part of a manufacturing ERP, through connected quality and warehouse applications, or as a specialised solution integrated with existing systems. The right architecture depends on the factory's current software, process complexity and required level of control.
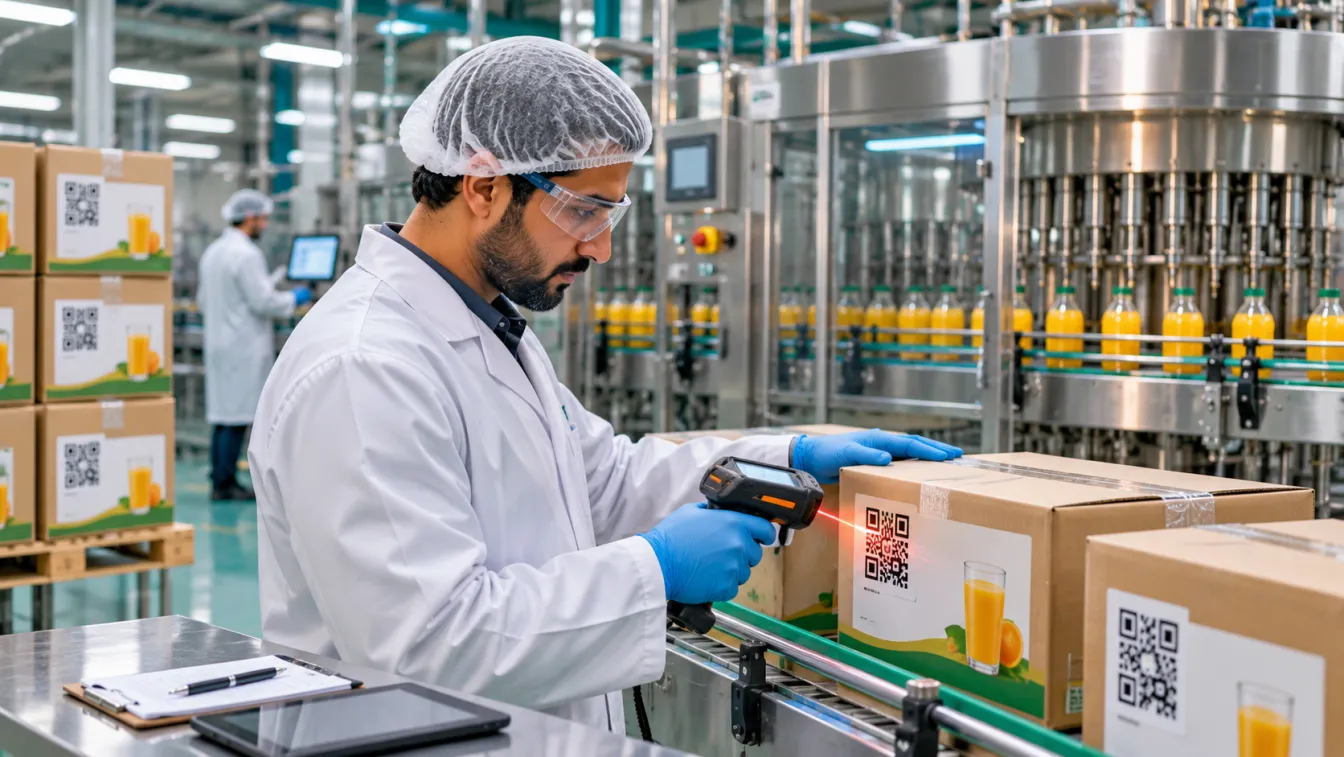
For many operations, barcode scanning is a practical starting point. Employees scan material labels during receiving, movement, issue and dispatch. QR codes can also provide a convenient way to retrieve batch details or supporting documents. RFID may be useful in selected environments where the operating conditions and asset or material characteristics justify it.
The important decision is not which label technology looks most advanced. It is whether the capture method fits the work. Scanning should be easy at the point of activity, labels should remain readable in the factory environment, and employees should have a clear alternative when a label is damaged or a device is unavailable.
Shop-floor tablets or terminals can capture production consumption, inspection results and batch completion. Where the factory already uses accounting, warehouse or production software, integration may be more appropriate than replacing every system. The architecture should establish which application owns each record and how updates are exchanged.
A custom solution can be useful when standard software cannot represent the factory's material transformations, split-and-merge rules, approval paths or machine-connected processes. However, customisation should follow documented requirements rather than being used to reproduce unclear manual practices.
How to implement traceability without disrupting production
A practical implementation begins with process mapping, not software configuration. Document how materials arrive, how lots are identified, where they are stored, how production consumes them and how finished goods are released and dispatched.
A phased approach can reduce implementation risk:
- Map the current process: Identify products, materials, locations, production stages, quality checks and the records currently used by each team.
- Define traceability requirements: Decide what must be traceable by lot, batch or serial number, which events must be recorded and who is responsible for each transaction.
- Clean master data: Review item codes, units of measure, supplier records, warehouse locations, bills of materials and existing lot conventions.
- Configure a representative workflow: Test receiving, inspection, storage, material issue, production consumption, finished-goods receipt and dispatch using realistic factory scenarios.
- Pilot with selected products: Run the process with a defined product group or production area. Compare system records with physical movements and investigate gaps.
- Train teams and expand: Train receiving, warehouse, production, quality and dispatch employees before extending the workflow to more products or locations.
Testing should include exceptions, not just the ideal process. Consider partial receipts, rejected deliveries, split lots, substituted materials, production rework, returned quantities, damaged labels and urgent dispatch requests. These are the situations that reveal whether the design reflects actual factory work.
Common traceability mistakes to avoid
One common mistake is recording a lot number only when material arrives. If subsequent movements and consumption are not captured, the factory cannot reliably establish where the material went.
Another is treating planned production inputs as proof of actual consumption. A bill of materials describes expected requirements, but operators may use approved alternatives, return unused quantities or record process losses. The system needs a practical way to capture what happened.
Factories can also create too many identifiers without defining ownership. Different teams may assign separate labels to the same material, making it difficult to connect records. Establish clear numbering rules and preserve supplier references.
Finally, do not assume that installing scanners will solve data-quality problems. Scanning improves capture only when employees follow a defined transaction process and the system validates the information. Training, clear responsibilities and routine reconciliation remain essential.
When is a factory ready to invest?
A factory may be ready when customer investigations take too long, material histories are spread across paper and spreadsheets, quality holds are difficult to enforce, or teams cannot confidently connect finished batches to their inputs. Repeated changes in product mix, suppliers or production locations can also expose weaknesses in manual tracking.
However, a factory does not necessarily need a complex custom platform immediately. If product and material identities are inconsistent, receiving is not recorded reliably, or employees do not follow basic inventory transactions, those foundations should be addressed first. Automating an undefined process can make errors faster without making the history more trustworthy.
Before selecting software, prepare a small set of real traceability scenarios. Ask a supplier-lot question and a finished-batch question. Confirm that the proposed solution can show the related receipts, movements, consumption, quality records and dispatches, including exceptions. Evaluate usability on the factory floor as carefully as reporting features.
For manufacturers considering a broader system, our guide to production planning software explains how production orders and schedules connect with material availability. Traceability should fit into that wider operating model rather than becoming another disconnected database.
Work with us: Whether you are evaluating manufacturing ERP in Riyadh, Jeddah or the Eastern Province, LtsThink helps Saudi manufacturers design connected production, inventory and quality workflows through a manufacturing ERP and MES solution. If you are reviewing how materials move through your factory, explore our guide to manufacturing inventory management or contact our team to discuss your processes.
FAQ
What is a manufacturing traceability system?
A manufacturing traceability system records and connects the identity and history of materials, production batches and finished products. It helps a factory trace inputs forward to shipments and finished products backward to their source materials.
What is the difference between forward and backward traceability?
Forward traceability starts with a supplier lot or material and identifies the production batches and shipments that used it. Backward traceability starts with a finished product or batch and identifies the materials, suppliers and production records behind it.
Do small and medium-sized factories need barcode scanning?
Not every factory needs the same technology. Some can begin with controlled lot records and reliable transaction entry. Barcode or QR scanning becomes useful when it makes receiving, movement, consumption and dispatch capture more accurate and practical.
Can traceability be added to an existing ERP system?
Often, yes. The feasibility depends on the existing ERP's inventory, production and quality capabilities, as well as its integration options. A review should identify which records can remain in the current system and where additional workflows or integrations are needed.